Fully certified medical examination and heavy-duty industrial nitrile gloves engineered for healthcare networks, chemical processing, automobile assembly, and regional trade hubs across Uzbekistan.
Analyzing the demand drivers, regulatory shifts, and industrial expansion in Central Asia's most populous market.
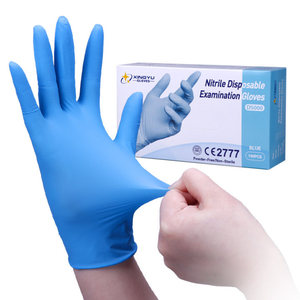
Under the national Presidential Decree on Healthcare Reform, Uzbekistan is rapidly expanding its hospital network, clinical diagnostic centers, and regional polyclinics across Tashkent, Samarkand, Andijan, and Fergana. This initiative has triggered an unprecedented surge in demand for medical-grade, powder-free nitrile examination gloves (CE Marked, ISO 13485) compliant with Ministry of Health regulations. Local buyers require consistent barrier protection against bloodborne pathogens, infectious fluids, and aggressive sterilizing agents.
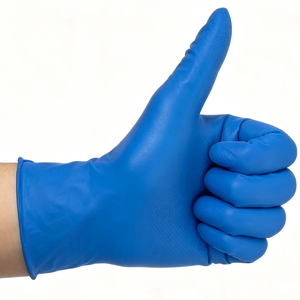
Uzbekistan’s robust industrial sector—anchored by the Navoi Mining and Metallurgical Combinat (NMMC), Almalyk MMC, UzAuto Motors manufacturing complexes, and extensive agro-processing plants in the Fergana Valley—demands high-tensile, chemical-resistant nitrile hand protection. Industrial buyers prioritize 6mil to 8mil diamond-textured nitrile gloves and nitrile-coated fabric safety gloves capable of withstanding petroleum hydrocarbons, solvents, agricultural chemicals, and abrasive mechanical wear.
B2B buyers in Uzbekistan face dry continental climate extremes, prolonged transit corridors, and rigorous customs inspection at post-clearance facilities. Successful suppliers must guarantee heat-stable chemical formulations, robust inner carton packaging, validated sterility release dossiers, and compliant Certificates of Origin (Form CT-1 or General Form A) to streamline clearance through Uzbekistan State Customs Committee checkpoints.
Comprehensive performance parameters for procurement directors, safety engineers, and regulatory officers.
Nitrile gloves are manufactured from Acrylonitrile-Butadiene Rubber (NBR), a synthetic copolymer offering superior chemical resilience, puncture strength, and allergy-free safety compared to natural rubber latex (NR) or polyvinyl chloride (PVC). For institutional procurement officers evaluating bulk glove shipments, understanding key physical metrics is essential for optimizing cost-per-unit against operational longevity.
| Performance Specification | Medical Exam Nitrile (CE / EN 455) | Heavy-Duty Industrial Nitrile (8 Mil) | Nitrile Coated Work Safety Gloves |
|---|---|---|---|
| Primary Material | 100% Synthetic NBR (Powder-Free) | High-Density NBR Compound | 13-Gauge Nylon/Polyester + NBR Coating |
| Thickness (Single Wall) | 3.5 mil – 5.0 mil (Palm) | 8.0 mil – 9.0 mil (Elevated Grip) | 1.1 mm – 1.3 mm (Coated Area) |
| Tensile Strength (Before Aging) | ≥ 14 MPa to 18 MPa | ≥ 21 MPa | Abrasion Level 4 (EN 388) |
| Elongation at Break | ≥ 500% | ≥ 450% | High Elasticity Liner |
| AQL (Acceptable Quality Level) | AQL 1.5 Freedom from Holes | AQL 2.5 / AQL 1.5 Industrial | EN 388: 4121X Safety Grade |
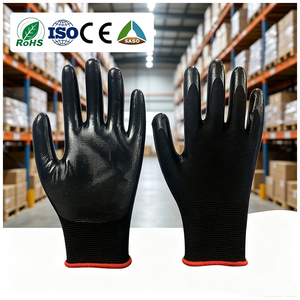
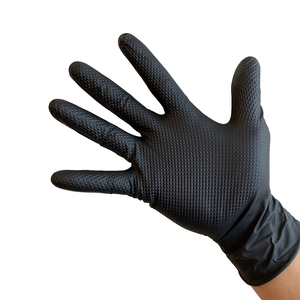
| Surface Texture | Micro-textured fingertips / Smooth | 3D Raised Diamond Pattern | Foam / Smooth Nitrile Palm Dip |
| Regulatory Approvals | EN 455 (1-4), ASTM D6319, ISO 13485 | EN ISO 374-1 (Type B), EN 420 | CE EN 388, EAC Compliance |
Nitrile synthetic elastomer provides an exceptional defense barrier against petroleum-based lubricants, diesel fuel, hydraulic oils, isopropyl alcohol, dilute acids, and alkaline cleaning liquids. Unlike natural latex, nitrile does not degrade when exposed to grease or heavy mineral oils, making it the material of choice for Uzbek automotive repair networks and chemical processing facilities.
Type I immediate hypersensitivity reactions associated with natural latex proteins present a major liability in medical and food service environments. 100% synthetic nitrile eliminates latex protein contamination risks completely, ensuring safe, long-duration wear for healthcare personnel in surgical wards, ICUs, and food processing lines.
Central Asian trade routes involve extreme thermal swings—from hot summer desert transits (+45°C) to cold winter warehousing (-15°C). Our proprietary vulcanization process prevents thermal degradation, blocking tackiness, embrittlement, or shelf-life shortening during container transport.
Tailored hand protection solutions matching specific industry demands across regional industrial hubs.
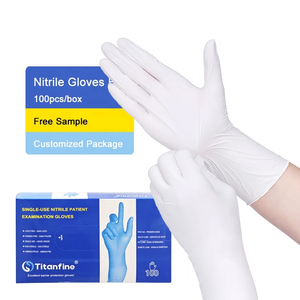
In major health clusters such as Tashkent City Medical Center and regional clinical hospitals in Bukhara and Samarkand, precision hand protection is vital. Our White & Blue Disposable Medical Nitrile Examination Gloves (5mil, CE Certified) provide tactile sensitivity for venipuncture, catheter placement, lab analysis, and surgical prep. The powder-free interior eliminates cornstarch contamination in diagnostic specimens.
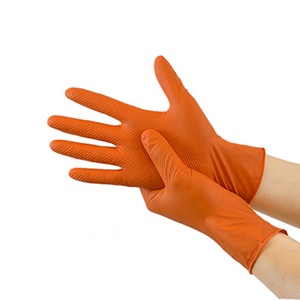
For heavy industrial complexes like Navoi Mining & Metallurgy Combinat (NMMC) and Almalyk MMC, standard thin disposables are inadequate. The 8 Mil Heavy Duty Orange & Black Nitrile Gloves with Raised Diamond Texture are designed specifically for heavy equipment servicing, conveyor belt repairs, and metallurgical refining processes.
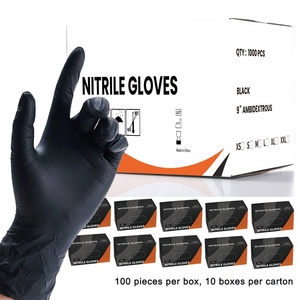
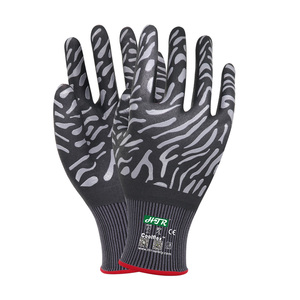
Supporting the auto supply chain in Asaka (Andijan region) and nationwide service franchises, automotive technicians encounter harsh solvents, brake fluids, and engine oil daily. Our Smooth 100% Black Nitrile Gloves and Nitrile Coated Work Safety Gloves offer the ideal combination of chemical protection, durability, and sleek aesthetics preferred by premium auto repair centers and detailers.
With Uzbekistan being a global exporter of dried fruits, fresh produce, and cotton products, hygienic food handling is paramount. Our Eco-Friendly Recycled Nitrile Work Gloves and food-contact-approved powder-free disposables serve agro-industrial packing houses and high-end hospitality venues throughout Tashkent, Khiva, and Samarkand.
Leveraging over three decades of medical device manufacturing experience to deliver uncompromised glove quality to Central Asian markets.
Production takes place inside controlled atmosphere ISO Class 7 and Class 8 cleanrooms equipped with positive differential pressure control, HEPA filtration, and strict gowning protocols to eliminate airborne particulate contamination during dipping, leaching, and inner box packaging.
Every shipment exported to Uzbekistan is traceable to raw polymer lot numbers, vulcanization temperatures, leaching water purity metrics, and automated pinhole detection records. Complete Certificates of Analysis (CoA) accompany every container.
We provide complete private label solutions tailored for Uzbek distributors. Our graphics desk assists with localized Russian and Uzbek language box printing, barcode integration, artwork proofing, and localized Ministry of Health compliant labelling.
Streamlined international transport pathways and customs clearance workflows for seamless delivery to Tashkent and beyond.
As Uzbekistan is a double-landlocked nation, established transit logistics are critical to prevent port delays or excessive demurrage fees. We offer established, cost-optimized shipping routes:
To clear customs through the State Customs Committee of Uzbekistan without administrative hold-ups, we supply a complete documentation package with every shipment:
Direct answers to common technical, logistics, and order management inquiries from wholesale procurement teams.
Partner with an established global exporter. Contact our dedicated Central Asian export sales department today for factory-direct pricing, technical datasheets, and sample dispatch.