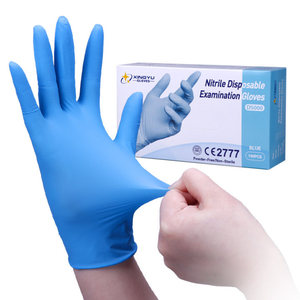
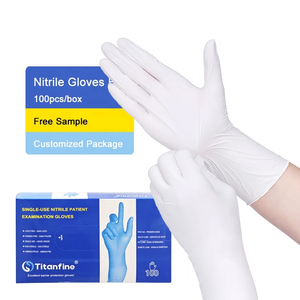
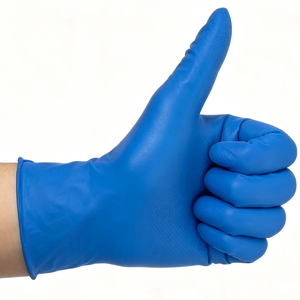
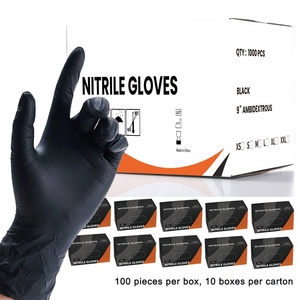
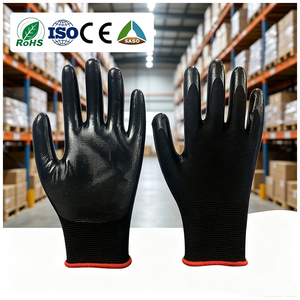
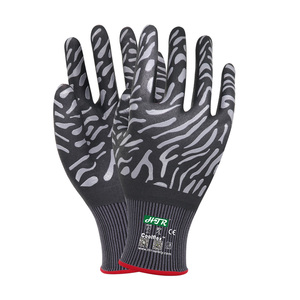
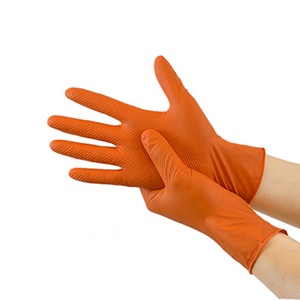
As a global pioneer in single-use barrier technology and specialized elastomer dipping, our manufacturing facility at Plot No. 4002, G.I.D.C., Phase-IV, Vatva, Ahmedabad, India (operated under Shree Umiya Surgical Pvt. Ltd. / Mediplus) delivers world-class medical disposable solutions. With over 36 years of industrial engineering excellence since 1988, we combine advanced Acrylonitrile Butadiene Rubber (NBR) compounding with ISO Class 7 & 8 cleanroom dipping environments to meet the stringent demands of international healthcare systems and industrial safety buyers.
Every consignment of nitrile gloves produced in our factory adheres strictly to EU MDR 2017/745 regulations, ISO 13485 quality systems, US FDA guidelines, and EN 455/EN 374 standards. Through 100% automated pinhole detection and chemical leaching control, we ensure an Acceptance Quality Limit (AQL) of 1.0 to 1.5 for medical examination lines and AQL 0.65 for critical surgical barrier applications.
Nitrile gloves are manufactured from a synthetic copolymer of acrylonitrile and butadiene. This chemical formulation provides three distinct structural advantages over traditional natural rubber latex (NRL) and polyvinyl chloride (PVC) vinyl gloves:
Strategic insights for hospital group purchasing organizations (GPOs), medical device importers, industrial safety distributors, and government tender authorities.
Global healthcare procurement officers are actively mitigating geopolitical risks by shifting away from single-region supply concentration. Indian manufacturing hubs, backed by robust chemical supply networks and automated dipping infrastructure, are rapidly becoming the preferred alternative for resilient, long-term B2B glove contracts.
Standard nitrile gloves utilize sulfur accelerators (such as thiurams, dithiocarbamates, and thiazoles) which can trigger Type IV delayed cutaneous allergies. The market is accelerating toward accelerator-free NBR formulations that utilize cross-linked zinc chemistry to guarantee zero chemical skin sensitization.
International tenders increasingly require verified Environmental, Social, and Governance (ESG) credentials. Factories integrating rooftop solar arrays, closed-loop water reclamation, and biodegradable packaging are securing preferred supplier status in North American and European procurement tenders.
Emerging material engineering breakthroughs defining the next decade of personal protective equipment (PPE) and clinical diagnostics.
Advanced chemical engineering has enabled ultra-thin 3.0 mil nitrile formulations that retain high tensile strength (≥ 18 MPa) while dramatically reducing hand fatigue during long surgical interventions or delicate laboratory pipetting.
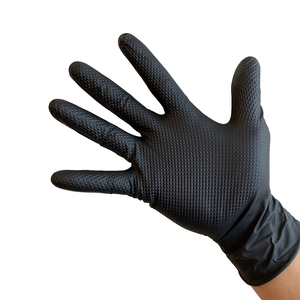
For industrial mechanics and heavy-duty automotive work, raised diamond texture patterns channel away fluids, greases, and heavy lubricants, creating maximum surface torque and reducing hand strain during heavy mechanical assembly.
High-tech electronics packaging and semiconductor assembly require ESD-safe nitrile formulations with surface resistivity between 10^9 and 10^11 ohms/sq, protecting sensitive microchips from electrostatic damage.
Operating under our parent organization Shree Umiya Surgical Pvt. Ltd. (Mediplus India), our manufacturing plant incorporates end-to-end quality controls—from raw NBR polymer compounding to cleanroom dipping, chlorine leaching, automated quality sorting, and sterile packaging.
We control every step from granule-to-carton. In-house compounding and high-speed double-former dipping lines eliminate third-party sub-assembly defects, ensuring lot-to-lot color, thickness, and tensile physical properties.
Our dedicated regulatory affairs division supplies complete technical files, Free Sale Certificates (FSC), ISO 10993 biocompatibility summaries, real-time stability reports, and CE certificates under EU MDR pathway for swift Ministry of Health approvals.
We provide custom inner box and outer shipper master carton printing, multilingual Instructions for Use (IFU), unique barcode/UDI generation, and buyer-defined pack sizes (e.g., 50, 100, or 200 gloves per box).
Our manufacturing facility is equipped with extensive rooftop solar power generation, minimizing environmental impact while ensuring stable, cost-efficient energy supplies for high-volume order fulfillment.
Technical and logistical insights for procurement managers, medical tenders, and wholesale importers.
Our manufacturing plant operates under a Quality Management System certified to ISO 13485 and ISO 9001. Our nitrile examination gloves carry CE mark certification under EU MDR regulations and adhere to international standards including EN 455 (Parts 1, 2, 3, 4), EN ISO 374 (Parts 1, 2, 4, 5), ASTM D6319 (for medical exam gloves), and ASTM D6978 (resistance to chemotherapy drugs). Every shipment is dispatched with batch-specific Certificates of Analysis (CoA).
AQL (Acceptance Quality Limit) defines the maximum allowable defect rate in a production batch. Medical grade nitrile gloves must achieve an AQL of 1.5 or stricter for water-tight pinhole tests, ensuring protection against blood-borne pathogens and viral transmission under EN 455-1. Industrial grade gloves generally target AQL 2.5 to 4.0, which is suitable for general cleaning, automotive repair, and food handling where barrier sterility is not legally mandated.
Yes, we offer complete OEM private-label branding services. Our design and compliance desk helps buyers prepare compliant packaging layout artwork, incorporating buyer branding, multilingual IFU instructions, regional distributor details, EAN/UPC barcodes, and Unique Device Identifier (UDI) data. Digital proofs are generated within 5 to 7 business days for buyer authorization prior to volume printing.
For standard catalogue nitrile gloves under factory branding, our minimum order quantity starts at 1 pallet per SKU. For custom OEM private-label packaging programmes, the standard MOQ is one 20-foot container (FCL), which can accommodate mixed sizes (S, M, L, XL). Regular production lead time is 3 to 4 weeks upon artwork approval and deposit confirmation. Ocean freight dispatches are routed through Mundra or Nhava Sheva ports under FOB, CFR, or CIF terms.
Our nitrile gloves undergo real-time and accelerated stability testing according to EN 455-4, validating a shelf-life of 3 to 5 years when stored in cool, dry conditions away from direct sunlight and ozone. Chemical breakthrough times are evaluated per EN ISO 374-1:2016 and ASTM F739 for key chemicals including n-Heptane, Sodium Hydroxide 40%, Sulfuric Acid 96%, Isopropanol, and Formaldehyde.
Absolutely. Our regulatory team routinely assists international distributors with MOH registration dossiers across Latin America, the Middle East, Africa, Southeast Asia, and CIS regions. We provide Free Sale Certificates (FSC), ISO 13485 & CE certificates, ISO 10993 biocompatibility summaries (cytotoxicity, sensitization, and primary skin irritation tests), technical data sheets (TDS), and legalized/apostilled legal documentation.
Request factory-direct wholesale quotations, technical product specification sheets, or schedule a virtual audit of our ISO 13485 cleanroom production lines today.